Views: 0 Author: Site Editor Publish Time: 2026-09-10 Origin: Site
Micro-stoppages in Surface Mount Technology (SMT) production lines compound rapidly, destroying daily output targets. Inefficient board feeding and handling errors cause these costly delays. Balancing high-speed throughput with zero-defect handling remains a major challenge for production engineers on the factory floor. Legacy feeding mechanisms frequently cause board jamming. They apply undue component stress and generate false sensor readings. These persistent issues halt the entire assembly line, forcing operators into constant troubleshooting loops. As the absolute first stage of the SMT line, the loading equipment dictates the pace. It establishes the takt time and sets the baseline reliability for all downstream processes. Evaluating a modern PCB Loader requires a deep understanding of its cycle mechanics. You must analyze sensor validation protocols and integration capabilities to ensure seamless operation and eliminate bottlenecks before they start.
Precision Cycle Mechanics: Modern loaders utilize advanced gas circuit designs and programmable pitch settings to eliminate board breakage and optimize magazine indexing.
Robust Sensor Validation: Reliable operation depends on precise optical and proximity sensor calibration, including correct mounting angles and continuous LED state verification.
Seamless Line Integration: True efficiency requires strict SMEMA compatibility and emerging Industry 4.0 connectivity, allowing the loader to communicate flawlessly with downstream printers, mounters, and factory execution systems.
Proactive Diagnostics: High-tier systems provide automatic fault code displays and accessible diagnostic interfaces to drastically reduce troubleshooting downtime.
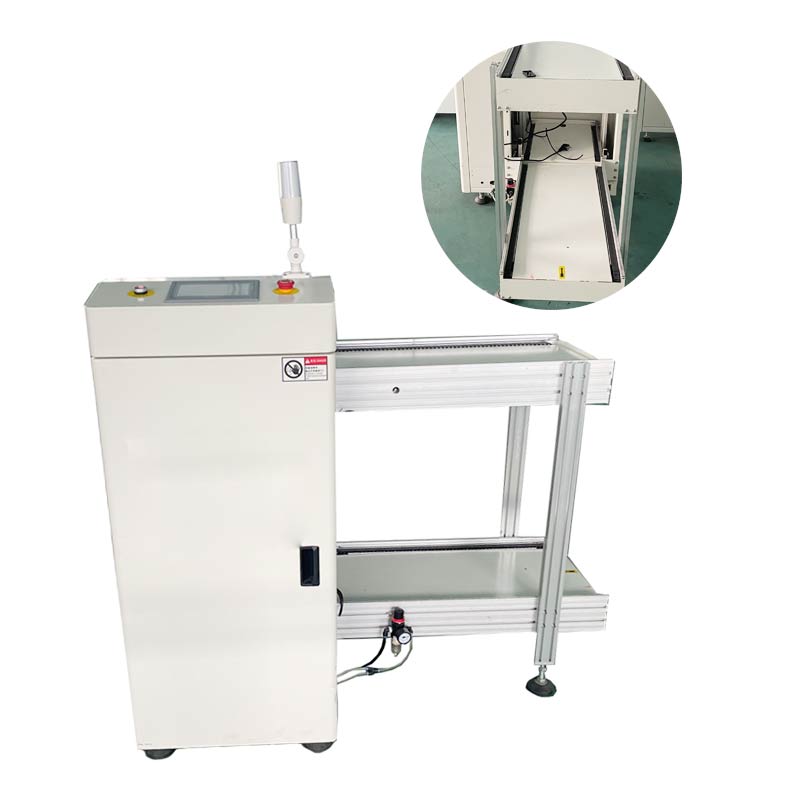
Standard magazine loaders handle double-sided or pre-assembled boards perfectly. They utilize slotted racks to keep individual substrates separated during the feeding process. This separation prevents bottom-side components from scraping against the board below them. Bare board stackers, destackers, and vacuum loaders optimize the feeding of raw, unpopulated PCBs. Choose the mechanical feeding type based on your specific assembly stage. Substrate fragility dictates the required handling method. Vacuum systems lift delicate boards without edge contact, using pneumatic suction cups to transfer the panel directly to the conveyor rails. Magazine racks provide secure slots for boards with existing bottom-side components. Selecting the wrong typology introduces immediate handling defects. A stacker will crush bottom-side components if used incorrectly. Conversely, using a magazine rack for raw, thin boards often leads to sagging and slot misalignment.
Loader Typology | Ideal Application | Handling Mechanism | Primary Limitation |
|---|---|---|---|
Magazine Loader | Double-sided boards, heavy backplanes | Pneumatic pusher extracts board from slotted rack | Requires manual loading of heavy magazines |
Vacuum Destacker | Raw, unpopulated bare boards | Suction cups lift the top board from a stack | Cannot handle boards with pre-mounted components |
Drop Stacker | Thick, rigid bare boards | Mechanical escapement drops the bottom board | High risk of edge damage on fragile substrates |
The operational cycle follows a strict step-by-step sequence. Every microsecond saved during this sequence improves overall line efficiency. The machine control logic monitors each step, refusing to advance until the previous motion completes successfully.
The operator loads a full magazine into the lower buffer zone and presses the start button.
Pneumatic clamps secure the magazine rack, ensuring it remains perfectly vertical.
The elevator mechanism performs pitch indexing to align the first programmed slot with the downstream conveyor rail.
A pusher mechanism extends, extracting the board smoothly from the magazine and sliding it onto the conveyor.
The system completes a downstream handoff, waiting for the solder paste printer to signal that it has received the board.
The elevator indexes to the next programmed slot, and the cycle repeats until the magazine is entirely empty.
Vertical magazine movement relies on either stepper or servo motors. Servo motors offer superior closed-loop positioning accuracy. They eliminate the risk of skipped steps that plague older stepper-driven systems. An encoder on the servo motor constantly feeds position data back to the PLC. Programmable pitch selection is critical for production flexibility. Operators can set pitches at 10mm, 20mm, 30mm, or 40mm. This accommodates varying component heights and board thicknesses. A board with tall electrolytic capacitors requires a 40mm pitch to clear the slot above it. Proper alignment prevents the pusher from striking the board edge at an angle. Misalignment by even a millimeter causes catastrophic board jamming. Heavy-duty ball screws and linear guide rails ensure the elevator platform remains perfectly level during indexing.
Traditional pneumatic pushers are cost-effective and offer standard reliability. They depend heavily on consistent factory air pressure. Fluctuations in air supply lead to erratic pushing speeds. If line pressure drops below 0.4 MPa, the cylinder extends too slowly, causing a takt time delay. If pressure spikes, the rod slams into the board edge. Motorized or servo-driven pushers deliver higher precision. They allow programmable velocity control during the push cycle. Servo pushers reduce maintenance requirements related to air leaks and cylinder seal degradation. They also improve cycle time efficiency by optimizing the return stroke speed. A motorized pusher can slow down just before contacting the board edge. It then accelerates through the transfer phase and retracts at maximum velocity.
Modern gas circuit innovations regulate pneumatic force precisely. This guarantees zero PCB breakage during the extraction phase. The regulated pressure applies just enough force to move the board. If mechanical resistance spikes, the system halts immediately. These designs mitigate the risks of warped boards jamming. They also prevent tightly slotted boards from wedging inside the magazine rack. Advanced flow control valves cushion the end of the cylinder stroke. This eliminates the harsh mechanical impacts that cause micro-cracks in sensitive ceramic components. Proper gas circuit calibration separates a high-yield process from a high-scrap operation. Install a dedicated digital pressure switch on the incoming air line to monitor this variable continuously.
A network of sensors acts as the central nervous system of the pcb loader machine. These sensors prevent misfeeds and catastrophic equipment collisions. They monitor every mechanical movement in real-time. Without accurate sensor feedback, blind mechanical operations destroy fragile substrates. The control logic relies entirely on these inputs to sequence the pneumatic valves and drive motors. A single failed sensor can paralyze the entire loading mechanism. Therefore, sensor redundancy and high-quality optical components are non-negotiable for high-volume manufacturing environments. Most systems utilize 24VDC logic, sending NPN or PNP signals directly to the main controller.
Diffuse reflective and through-beam photoelectric sensors confirm board availability. They detect the edge of the PCB in the active magazine slot. Through-beam sensors are highly effective for detecting warped boards that might evade a diffuse sensor. Dark-colored solder masks absorb infrared light. Standard diffuse sensors often fail to detect matte black or dark blue PCBs. You must use background suppression sensors or through-beam configurations for these substrates. The system also validates the pusher's home and extended positions. Magnetic cylinder sensors verify that the pusher fully extends and retracts. This ensures complete board transfer before the magazine indexes to the next slot. If the pusher fails to return home, the elevator remains locked. This prevents the moving magazine from shearing the extended pusher rod.
Proximity sensors verify correct magazine seating. They ensure the rack is fully clamped before the cycle initiates. If a magazine sits unevenly, the sensors inhibit the start command. Safety sensor protocols protect both the product and the operator. Area scanners or physical door interlocks halt operation instantly. They trigger if a magazine is improperly loaded or if operator interference occurs. Redundant safety relays ensure that opening a guarding door cuts power to the drive motors immediately. This compliance with industrial safety standards prevents severe workplace injuries.
Sensor Type | Application | Detection Method | Common Failure Mode |
|---|---|---|---|
Diffuse Reflective | Board presence in slot | Light bounces off PCB | Dark solder mask absorbs light |
Through-Beam | Magazine rack alignment | Light breaks across gap | Dust blocks the emitter lens |
Magnetic Reed | Pneumatic cylinder position | Detects internal magnet | Vibration shifts the sensor position |
Inductive Proximity | Safety door interlock | Metal detection | Physical impact breaks the housing |
Modern interfaces have transitioned from simple alarm lights to comprehensive HMI touchscreens. These screens feature automatic fault code generation. Real-time diagnostic feedback accelerates troubleshooting. It identifies specific sensor failures or mechanical blockages immediately. Operators no longer guess which sensor caused the stoppage. The HMI displays a visual map of the machine, highlighting the exact sensor that failed to trigger. This level of diagnostic transparency reduces mean time to repair (MTTR) from hours to mere minutes. It empowers line operators to resolve minor faults without calling maintenance technicians.
Standard SMEMA interfaces dictate the electrical handshake between machines. The protocol relies on a simple dry contact relay system. The upstream machine closes a relay to signal 'Board Available'. The downstream machine closes a relay to signal 'Machine Ready'. When both relays are closed, the board transfers. This prevents collisions on the conveyor. Strict adherence to SMEMA protocols eliminates complex custom wiring. It ensures that integrating a new smt pcb loader takes minutes rather than days. The standard pinout uses Pin 1 and 2 for the Board Available signal, and Pin 3 and 4 for the Machine Ready signal.
Future trends in loader technology emphasize Industry 4.0 connectivity. IoT sensor integration allows for advanced predictive maintenance. Modern loaders interface directly with Manufacturing Execution Systems (MES) using SECS/GEM protocols or standard RJ45 Ethernet ports. This provides real-time traceability and accurate yield tracking. Remote line management becomes possible, allowing supervisors to monitor magazine status from a central dashboard. Machines now broadcast their operational status, fault history, and cycle counts to factory servers. This data-driven approach transforms a simple feeding mechanism into an intelligent node within the smart factory network.
Facilities must compare standard-sized machines with compact models. Mini loaders are designed specifically for space-constrained environments. They provide the same functionality while consuming half the floor space, allowing for tighter aisle configurations. Customization options expand operational capabilities significantly. Dual-magazine capacities reduce operator intervention frequency. Heavy-duty configurations handle thick, heavy backplanes easily. Adjustable rail widths accommodate diverse product portfolios. Facilities running high-mix, low-volume production benefit immensely from automated rail width adjustments. This feature eliminates the need for operators to manually crank handwheels during product changeovers.
Engineers must balance raw throughput with handling accuracy. Pushing boards too fast damages fragile or pre-assembled substrates. Gentle, accurate handling prevents micro-cracks in sensitive components. Integrating an automatic pcb unloader at the end of the line mirrors these exact requirements. It maintains a balanced line takt time by receiving boards just as carefully as they were loaded. The unloader must index its magazine precisely to catch the finished board without scraping the bottom-side solder joints. Matching the cycle times of both the loader and unloader ensures the SMT line never starves for raw boards or backs up with finished products.
False positives and negatives frequently plague SMT environments. Dust, solder paste, and flux residue coat sensor lenses over time. Establish strict protocols to clean the sensor face regularly. Verify the mounting angle to ensure the beam hits the target squarely. Confirm that the sensor LED lights up correctly during board passage. A flickering LED indicates a marginal detection threshold. Technicians must adjust the sensor sensitivity potentiometer to ensure solid detection regardless of board color. Turn the dial clockwise to increase sensitivity for dark boards, and counter-clockwise to reduce glare from highly reflective HASL finishes.
Warped PCBs and degraded plastic magazines cause binding during the push cycle. This mechanical stress damages board edges and stalls the pusher. Perform routine checks on pusher alignment using a dial indicator. Monitor magazine clamping pressure to ensure the rack remains perfectly vertical. Discard warped magazines immediately to prevent recurring jams. Heat cycling in curing ovens degrades plastic magazines over time. They lose their dimensional stability and pinch the boards. Standard magazines feature adjustable side plates. Operators turn a lead screw to widen or narrow the slots. Over time, the plastic slots wear down. A 1.6mm thick FR4 board might slip out of a worn slot and jam the elevator. Inspect magazines quarterly with a go/no-go gauge.
A realistic preventative maintenance framework ensures continuous uptime. Neglecting routine maintenance leads to erratic indexing and premature component failure. Implementing a structured schedule extends the lifespan of the equipment significantly. Keep replacement belts, sensors, and pneumatic seals in your local spare parts inventory to minimize downtime.
Maintenance Frequency | Component | Action Required |
|---|---|---|
Daily | Optical Sensors | Wipe lenses with isopropyl alcohol to remove dust and flux residue. |
Daily | Pneumatic System | Verify incoming air pressure matches manufacturer specifications (typically 0.4 - 0.6 MPa). Drain moisture traps. |
Weekly | Lead Screws & Guide Rails | Clean old grease and apply fresh lithium-based lubricant to prevent micro-vibrations. |
Weekly | Drive Belts | Inspect for fraying and verify correct tension to ensure accurate elevator indexing. |
Monthly | Pneumatic Cylinders | Inspect seals for air leaks and test the smooth actuation of the pusher mechanism. |
Quarterly | Magazine Racks | Measure slot width with calipers to check for wear. Discard distorted racks. |
Take the following actions to upgrade your board feeding process and eliminate line stoppages:
Audit your current line takt time to identify exact feeding bottlenecks.
Measure your available floor space to determine if a standard or mini model fits best.
Request specific sensor reliability data from potential equipment manufacturers.
Review SMEMA integration manuals to ensure compatibility with your existing printers and mounters.
Establish a strict preventative maintenance schedule before commissioning the new equipment.
A: It automatically feeds bare or partially assembled printed circuit boards into the SMT production line. It extracts boards from a magazine rack and transfers them to the downstream solder paste printer or conveyor, establishing the initial takt time.
A: A magazine loader uses slotted racks to hold separated boards, making it ideal for double-sided assemblies. A vacuum stacker lifts raw, unpopulated boards directly from a stacked pile using suction cups, optimizing space for bare board feeding.
A: It utilizes advanced gas circuit designs and precise pneumatic regulators. These systems control the pushing force. If the pusher encounters abnormal resistance from a jammed or warped board, the system halts immediately to prevent physical damage.
A: Environmental contamination is the leading cause. Dust, solder paste, and flux residue accumulate on the optical sensor lenses. This blocks the light beam, causing false negatives or false positives during board detection.
A: First, clean the sensor face with isopropyl alcohol. Next, verify the mounting angle is perpendicular to the target. Finally, check the sensor's LED indicator and adjust the sensitivity dial to account for dark-colored solder masks.
A: SMEMA is an industry-standard electrical interface protocol. It allows different brands of SMT equipment to communicate. It uses "Board Available" and "Machine Ready" signals to ensure safe, synchronized board transfers between machines without collisions.